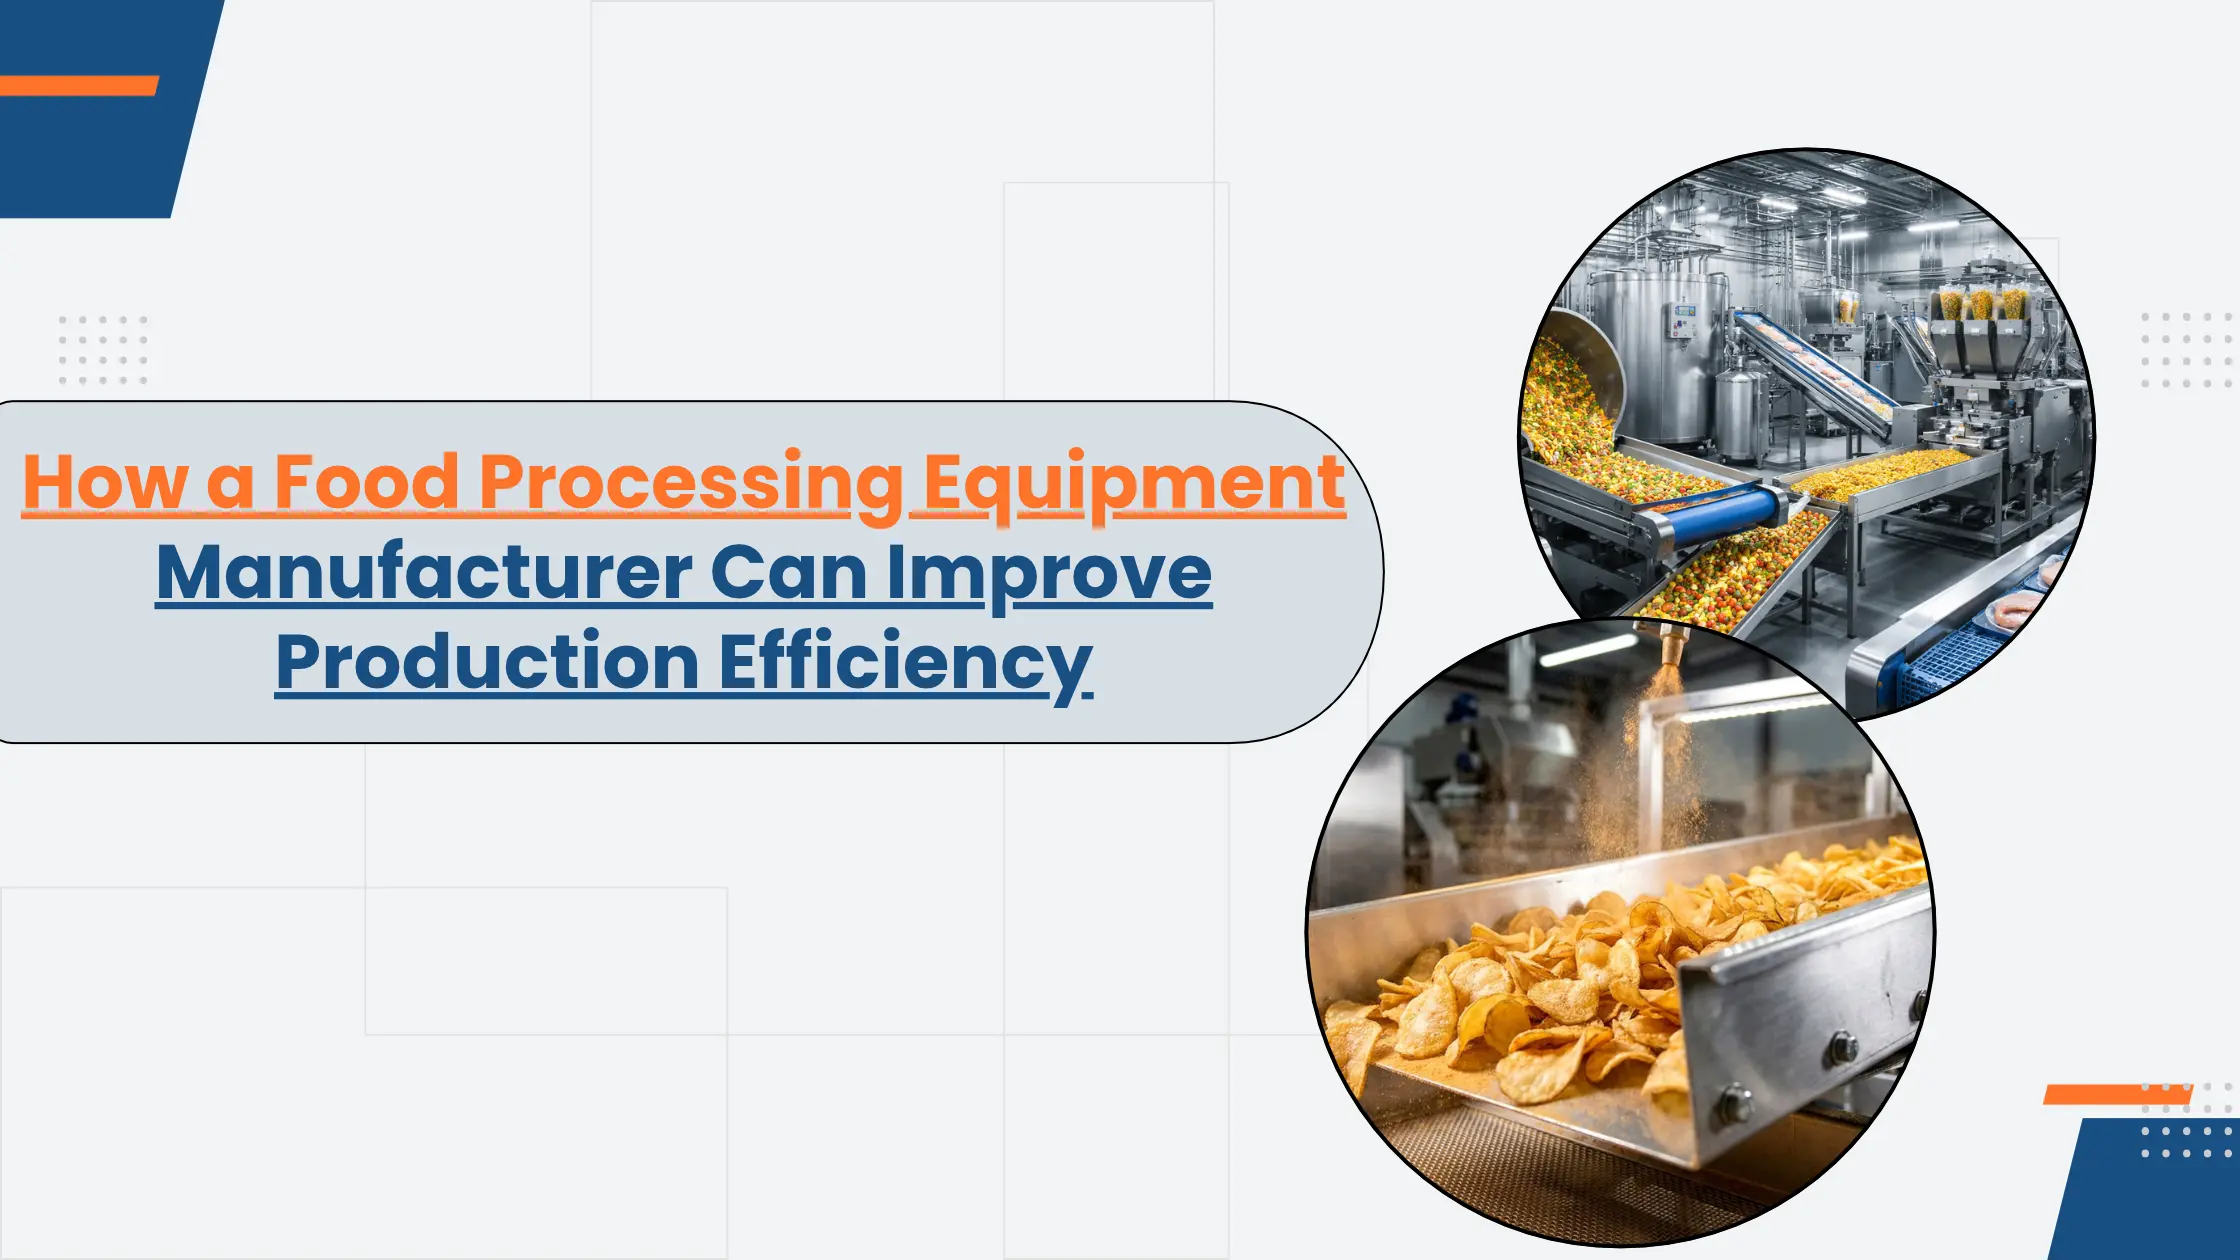
Efficient food processing requires clean, sterile equipment; the process involves several stages in which raw materials are screened, graded, fed into other containers, moved, and handled consistently. The increasing production requirements make it necessary to get equipment that can support efficient material handling while maintaining product quality and hygiene.
This is where a food processing equipment manufacturer helps. The right vibratory equipment from them can improve screening accuracy, maintain consistent material flow, control ingredient feeding, and support efficient packaging operation.
In this guide, let’s learn how food processing machine manufacturers help improve production efficiency.
Understanding Food Processing Equipment
Food manufacturing equipment is machinery used for handling and processing food products and ingredients during different stages of production and manufacturing. Depending on the application, they can be used for screening, separating, feeding, moving, etc.
Vibratory equipment such as a vibratory feeder and vibratory table uses controlled vibration to perform these functions. For example, a vibratory feeder can provide controlled feeding, while a vibratory separator can separate particles according to their size.
Different stages of processing need different equipment; moreover, choosing the right equipment depends on the material being handled and the other specific requirements of the production process.
Different Types of Food Processing Machines
For different material handling requirements, there are different vibratory solutions such as:
These separators are used for accurate screening and grading of fine and ultra-fine materials such as flour, spice, and sugar screening. They are also known as a floor screening machine.
Horizontal screen separators are designed for high-capacity screening; for example, they can be used for grain grading, dedusting, and de-stoning.
These feeders are used for ingredient dosing and feeding onto processing and packaging lines. Whether the material is powder or granules, vibratory feeders provide controlled and consistent feeding.
Installed on bins, hoppers, and storage units, these bin vibrators assist the flow of bulk material and address problems such as rat-holing and bridging to support consistent material discharge.
Vibratory tables, also known as compaction tables, are used to settle powders and granular products into containers during final packaging. They help improve fill rate, remove trapped air, and improve presentation and net-weight consistency.
These motors provide the vibratory force required by other vibratory equipment. For example, in a flour screening machine, these motors help create the movement required for separating and grading materials.
How Food Processing Equipment Manufacturers Improve Production Efficiency
The role of a food processing plant equipment manufacturer is not just about supplying robust machines. Instead, the right manufacturer will understand your material, production requirements, and operating conditions to provide equipment that meets your application needs.
Here are some examples of how these manufacturers improve food processing production efficiency:
Improving Screening Accuracy
Screening accuracy is important when processing materials like flour, grain, spices, and fine powders. The appropriate screening equipment helps separate the particles according to the required size. For example, a gyratory screen separator uses spiral vibratory motion to provide thorough particle-to-mesh contact; it is suitable for accurate screening of flour, powder, and spice.
Supporting High-Capacity Grain Processing
Grain-processing operations need to handle large quantities of material while maintaining a consistent screening performance. That’s where a horizontal screen separator comes into play; it is suitable for applications where grains need to be processed at higher capacity.
Providing Controlled Ingredient Feeding
As irregular feeding affects the material flow and batching, ingredients need to be supplied to processing lines at a consistent rate. Vibratory feeders help provide a controlled and uniform dosing of powders and granular materials onto processing lines, to support steady feed rate and accurate batching.
Improving Material Flow From Bins and Hoppers
Food powders and granular materials sometimes have difficulty flowing from storage bins or hoppers. That’s where bin vibrators are used; their controlled vibrations eliminate bridging and rat-holing. They support consistent, gravity-assisted flow of fine powders to maintain material movement between storage and the next stage of processing.
Improving Fill Accuracy During Packaging
Efficiency matters even during the final stage of packaging. Uneven settlement of powder and granular materials into containers can affect the amount of material that fits inside them. Through a compaction table, this problem is treated; the vibration from this table settles the material and removes trapped air, improving fill accuracy and net-weight consistency.
Supporting Hygienic Food Processing
Hygiene is an uncompromised aspect of food processing; that’s why industrial food processing equipment is designed to support hygiene by minimising areas where food can accumulate. For example, food processing machines at Vibro Flux highlight food-grade materials and hygienic design practices.
Supporting Continuous Production
The key benefit of vibratory equipment in food processing is that they support continuous production. These machines operate reliably during continuous production by maintaining consistency between different stages of production and reducing interruptions caused by material handling problems.
Check Out Reliable Food Processing Solutions at Vibro Flux
Vibro Flux is India’s leading food processing equipment manufacturer, where we provide equipment designed specifically for food processing applications. Our equipment range includes gyratory screen separators, horizontal screen separators, vibrating feeders, bin/hopper vibrators, compaction tables, and vibratory motors.
Each machine supports a different application, such as flour and grain screening, spice and powder sieving, dairy powder separation, sugar and confectionery grading, ingredient dosing, and final packaging.
Final Thoughts
The right vibratory equipment improves production efficiency in food processing by providing accurate screening for high-capacity grain processing, controlled feeding, improved material flow, and packaging settlement.
However, the effectiveness of these machines depends on several factors, one of which is choosing the right manufacturer. The correct manufacturer will provide suitable vibratory solutions, customisation options, food-grade construction, and after sales technical support.
Get in touch with us at Vibro Flux, where we provide professional guidance and help you find the right equipment solution!